Types of Printing Process Materials
Paper and Fibrous Materials
Paper
Paper is a fiber-based material produced from wood, rags or organic material. The types of paper used in the packaging and graphic arts industries typically use wood and/or recycled paper and board, which is then chemically or mechanically processed to produce cellulose pulp. This pulp is bleached and processed in a paper making machine to produce reels of paper which may optionally be coated or finished to provide a better surface and/or improved visual appearance.
Paper may be between 0.07 mm and 0.18mm thick, with paper for printing and packaging applications generally being in a range between 60 and 120 gsm. The crossover point between paper and board is normally considered to be around 160 grams per square meter (gsm), as it is only at this level that a fibrous material is likely to be stiff and rigid enough to make a container.
Paper has a wide range of industrial applications including use for the packaging of products as diverse as confectionery and cigarettes, as a component in packaging laminates, and for many commercial print uses.
Carton Board
Carton board (also called cardboard, paperboard or solid board) is the name for a range of paper based materials that includes folding box board (FBB, GC or UC), solid bleached board (SBB, SBS, or GZ), solid unbleached board (SUB or SUS), white lined chipboards (WLC, GD, GT, or UD), some unlined chipboards, and certain laminated boards.
To manufacture carton board, fibrous material, either from trees, recycled paper, or a mixture of the two, is turned into pulp. It is then bleached and processed in a board making machine to create a board consisting of one or more layers, which may optionally be coated to provide a better surface and/or improved visual appearance.
The crossover point between paper and board is normally considered to be around 160 grams per square meter (gsm), as it is only at this level that a fibrous material is likely to be stiff and rigid enough to make a container.
Carton board is primarily used in the packaging industry to produce all types of folding cartons but may also be used for graphics applications. For folding cartons the board used will normally be in the range 200 to 600gsm, or 350 to 800 microns.
Specialized and Corrugated Boards
Corrugated Board
Corrugated board is manufactured by combining lining paper with a fluting medium in a unit called a single facer. The liners used may be made from recycled, test, or kraft papers, and will consequently have a brown or white surface, which may be coated or semi-coated, depending on the application they are to be used for. Fluting medium is generally recycled paper.
In the single facer unit, heat, steam, and a corrugating roller are used to corrugate the fluting medium, which then has the liner attached. This creates single face, the basic building block of all corrugated board. Single face is used 'as is' for some specific applications such as litho-lamination, but is normally combined with further liners and fluting media to produce single wall corrugated (single face plus a top liner), double wall (single wall plus single face), or multi-wall (further combinations of the above).
The thickness of the corrugated material will depend on the fluting height created by the single facer and the combination of flutings used. The range of thicknesses can vary from 0,5 mm for the finest, up to 15 mm for the thickest, and sometimes more. The most commonly used grammages are in the range from 80 gsm to 300 gsm, however for some specific applications lighter or heavier papers may be used.
Heavy Solid Board
Heavy solid board is a type of carton board with a high basis weight.
To manufacture heavy solid board, fibrous material, either from trees, recycled paper, or a mixture of the two, is turned into pulp. It is then bleached and processed in a board making machine to create a board consisting of one or more layers, which may optionally be coated to provide a better surface and/or improved visual appearance. The resulting board will normally be heavier than 1000 grams per square meter (gsm).
Heavy solid board is primarily used in the packaging industry for applications where a high level of mechanical strength is required, such as trays for meat products or puzzle.
Synthetic and Plastic Packaging Materials
Semi-Rigid Plastics
Today’s converters have a wide choice of plastic materials available, including products such as Polypropylene (PP), Polyethylene (PE), Polyvinylchloride (PVC), Polyesterterephtalate (PET), and more recently, Polylactic acid (PLA) which is made from renewable sources.
For some years there has been a level of transition by packaging specifiers from traditional cardboard to plastics, particularly in the area of cosmetic and luxury packaging.
One of the major benefits of plastic packaging is to be found in its high “performance/weight” ratio, its lightness (which enables savings in transportation), and its high calorific value which improves its efficiency of incineration.
Transparent and semi-transparent packaging tends to be associated with luxury or high added-value products, and the versatility and design flexibility that plastics offer can give life to packaging that will stand out among rival products.
The movement toward these materials has been driven by the specific features and benefits which plastics bring to high-end packaging applications, including:
- allowing the customer to see the product inside and to check the contents easily
- specialized effects with full or partial visibility
- glossy finishes that add interest to the package
- moisture resistance
- excellent coloring ability
- good folding and die-cutting properties
- recyclability
Film
A film is usually characterized as a thin synthetic resin layer. There are many types of films and their use depends on their physical and chemical properties, which make them especially suitable for a given application.
The most commonly used plastic films are low density polyethylene (LDPE), Polypropylene (PP), bi-oriented polypropylene (BOPP), and polyester (PET).
Printed film is used for packaging, display materials, label stickers, seals, and a wide range of other graphic applications.
Films are generally characterized by their basis weight, expressed in g/m²; and thickness, expressed in microns. For some films it is also useful to know their density, expressed in g/cm3.
The increasing awareness of environmental issues is intensifying research into film substrates derived from renewable sources that are compostable.
Learn More About
What is High Speed Paper Roll to Sheet Cutting Machine?
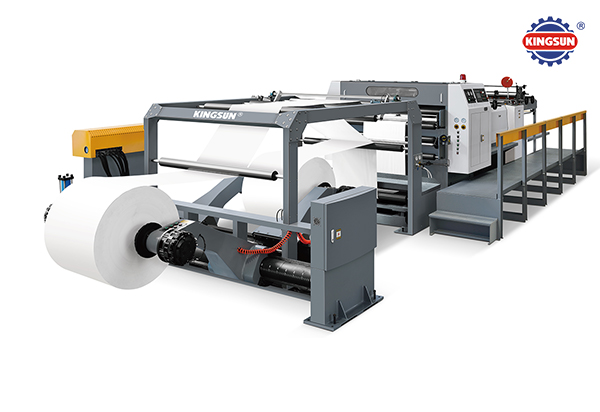
The high-speed paper roll to sheet cutting machine is kind of equipment specially designed for jumbo roll paper slitting and cutting into sheet paper. The thickness of the converting paper is between 50-650gsm. After processing, the cut paper can go directly to print on an offset press or to cut again on guillotine according to the actual situation. It is the most efficient equipment for web paper converting. It can also be called a high-speed paper roll sheet cutter. Currently, it is widely used for the paper industry, the printing industry, the paper trade industry. It is different from the slitter rewinder (just slitting) and the paper cutter(guillotine).
Offset vs. Flexo Printing
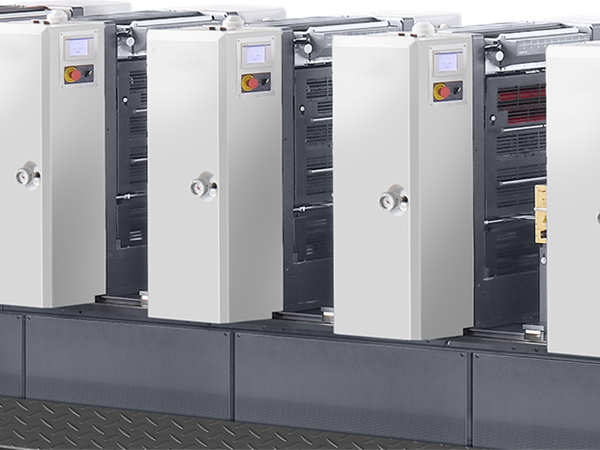
In the modern label printing industry, offset and flexographic printing are two widely used mainstream printing methods. Each brings its own unique technical characteristics and application advantages, playing crucial roles in different production scenarios. This article will systematically compare these two printing technologies from various angles, including printing principles, technical strengths, application limitations, cost structures, and selection recommendations - to provide professional guidance for label printing and converting businesses like yours when choosing a suitable process. 1. Differences in Printing Principles and Technical Characteristics Offset Printing uses an indirect printing principle, transferring images and text from the printing plate to a rubber blanket cylinder before applying them to the substrate. Its key features include: • Ink-Water Balance System: Relies on precise control of the ink-water balance, leveraging the immiscibility of oil and water to transfer graphics and text. • Fine Dot Reproduction: Utilizes amplitude-modulated or frequency-modulated dots, achieving a printing resolution of 200–350 dpi. • Dependence on UV Curing: In label printing, UV curing systems are often required to ensure ink adhesion on non-absorbent materials. Flexo Printing, on the other hand, employs a direct relief printing method: • Anilox Roller Ink Transfer System: Uses engraved anilox rollers to precisely control ink transfer, ensuring consistent ink layer thickness. • Wide Printing Adaptability: Supports various ink systems, including water-based, solvent-based, and UV inks, offering flexible curing options. • Strong Material Compatibility: Particularly well-suited for handling non-absorbent materials like films and self-adhesive substrates. 2. Quality Performance and Process Advantages Three Main Advantages of Offset Printing 1. Superior Print Quality Offset printing has a natural advantage in reproducing fine details. Its dot density can reach 200–350 dots per inch, far exceeding the 170–180 dpi limit of flexo printing. This high precision makes it stand out in the following scenarios: • Smooth gradient transitions with no noticeable banding • Crisp edges on small text (below 4 pt) • Accurate spot color reproduction with high hue stability • Dot loss in highlight areas below 2% 2. Significant Initial Cost Advantages At the start of a new project, offset printing demonstrates clear economic benefits: • Lower Plate Costs: A set of four-color PS plates costs only 1/4 to 1/2 of flexographic resin plates. • Higher Plate-Making Efficiency: The CTP plate-making process takes just 8–12 minutes, compared to 60–90 minutes for flexographic plates. • Faster Job Changeovers: Standard job changeovers can be completed within 15 minutes, improving equipment utilization. 3. Higher Operational Tolerance Offset printing offers relatively stable performance characteristics: • The ink-water balance system has self-adjusting capabilities. • Dot gain is kept within standard ranges (typically 12–18%). • Even with less experienced operators, basic print quality can be maintained. Differentiated Advantages of Flexographic Printing 1. Wide Material Adaptability Flexographic printing excels in handling special materials: • Wide printable thickness range (0.012–0.5 mm) • Compatible with various film materials like PE, PP, PET, and BOPP • Supports special substrates such as metal foils, synthetic paper, and specialty papers 2. Potential for Higher Production Efficiency In specific applications, flexographic printing offers unique advantages: • Strong inline processing capabilities, integrating processes like foiling, laminating, die-cutting, slitting and sheeting. • Printing speeds of 150–300 meters per minute. • Suitable for long-run jobs, with operational costs decreasing as volume increases. 3. Superior Environmental Performance Modern flexographic technology aligns with green printing trends: • Lower VOC emissions from water-based inks compared to offset inks • Higher usage of biodegradable materials • Relatively lower energy consumption, meeting sustainability requirements 3. In-Depth Analysis of Cost Structures Equipment Investment Comparison The complex structure of offset presses leads to higher initial investment: • Inking System: Requires a precise ink transfer system with 12–20 ink rollers. • Dampening System: Equipped with automatic alcohol concentration control. • Registration System: Demands extremely high mechanical machining precision. • Overall, offset equipment is 30–40% more expensive than similarly configured flexographic printing equipment. Operational Cost Differences Consumable Costs: • Offset: PS plates cost ¥80–120 per square meter (this is roughly number, every year it will be change), with higher dampening solution consumption. • Flexo: Resin plates cost ¥200–350 per square meter (this is roughly number, depends on types, thickness and quality), and anilox rollers require periodic replacement. Energy Consumption Comparison: • Offset: UV curing systems consume more energy, using 15–25 kW per hour. • Flexo: Hot air-drying systems are relatively more energy-efficient, using 8–15 kW per hour. Labor Cost Considerations: • Offset: Requires experienced press operators with 6–12 months of training. • Flexo: Operators have shorter training cycles, typically becoming proficient in 3–6 months. 4. Recommendations for Application Scenarios Scenarios Favoring Offset Printing 1. High-Quality Commercial Labels: Cosmetics, luxury labels, and others requiring high-precision printing. 2. Short-Run Variable Data: Promotional labels or seasonal product labels requiring frequent plate changes. 3. Paper-Based Materials: Primarily using absorbent materials like coated paper or specialty paper. 4. Budget-Constrained Projects: Limited initial investment but with certain quality requirements. Scenarios Favoring Flexographic Printing 1. Film-Based Labels: Food packaging, daily chemical product labels, and others using film materials extensively. 2. Long-Run Production Tasks: Routine label production with volumes exceeding 100,000 meters. 3. Special Process Requirements: Situations needing inline processing or special ink applications. 4. Strict Environmental Requirements: Compliance with food-grade safety standards or environmental certifications. 5. Technological Trends and Integrated Innovations Today’s label printing technology is evolving toward integration: 1. Hybrid Printing Technology: Combines offset and flexographic units to balance fine details and large solid areas. 2. Digital Printing Integration: Incorporates digital inkjet units into traditional printing for variable data capabilities. 3. Intelligent Upgrades: Adoption of AI color management systems and IoT remote monitoring. 4. Green Transformation: Increased use of eco-friendly materials like vegetable oil-based inks and water-based coatings. 6. Key Factors for Decision-Making When choosing a printing process, your label business should consider: 1. Product Structure Analysis: The material types, design complexity, and quality requirements of your main label products. 2. Order Characteristics Evaluation: Average order volume, job changeover frequency, and delivery timelines. 3. Return on Investment Calculation: Comprehensive assessment of equipment depreciation, material costs, and labor expenses. 4. Technological Development Outlook: Evaluating upgrade potential and future business expansion needs. In Conclusion In the label printing industry, offset and flexographic printing each have their strengths, with no absolute winner. Offset printing holds a significant position in high-precision printing due to its superior print quality and lower startup costs. Meanwhile, flexographic printing offers unique advantages in packaging labels, thanks to its wide material adaptability and efficient production capabilities. A wise choice should be based on a thorough analysis of your own label business characteristics. If your work primarily involves paper-based materials, short runs, and high-quality requirements, offset printing may be the better fit. If it involves extensive use of film materials, long production runs, or special process needs, flexo printing will likely deliver greater value. As printing technology continues to develop, the boundaries between these two processes are gradually blurring, paving the way for more integrated and innovative solutions. Your business should stay technologically aware, flexibly adjust its technical approach based on market changes and customer needs, and find the optimal balance among quality, cost, and efficiency to gain a competitive edge in this dynamic label printing and converting market.
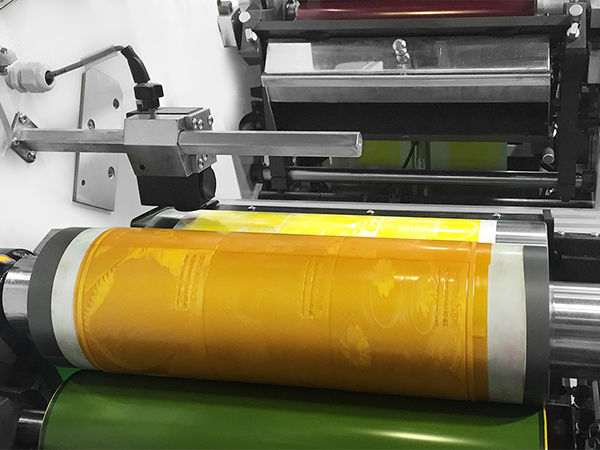
Label Flexographic Printing Presses Technical Features and Application
This article introduces label flexographic presses, highlighting their high speed, precision, modular design, and versatile inline processing for diverse materials and inks. It compares inline, CI, and stacked presses for short-run flexibility, long-run accuracy, and compact setups. Recommendations include analyzing product mix, order types, and future needs, and testing the label production equipment for optimal selection.